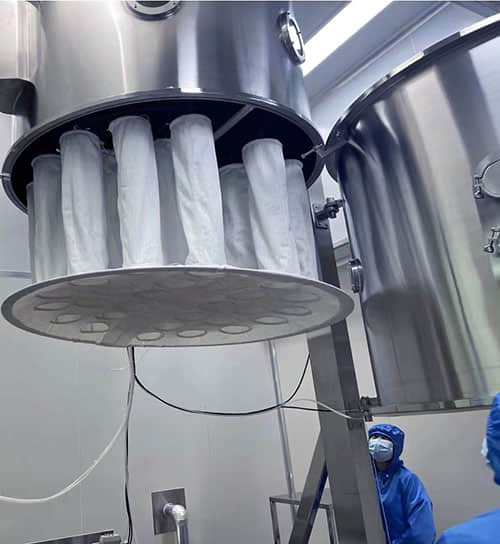
Powder Transfer System: The Ultimate Guide to Efficient Powder Handling
Introduction
In industries like pharmaceuticals, food processing, and chemical manufacturing, efficient powder transfer is crucial for maintaining product quality, safety, and operational efficiency. A powder transfer system is designed to move bulk powders seamlessly while minimizing contamination, dust exposure, and material loss.
In this article, we’ll explore what a powder transfer system is, its benefits, types, applications, and how to choose the best system for your needs. By optimizing powder handling, businesses can increase productivity and meet stringent industry regulations.
I. What is a Powder Transfer System?
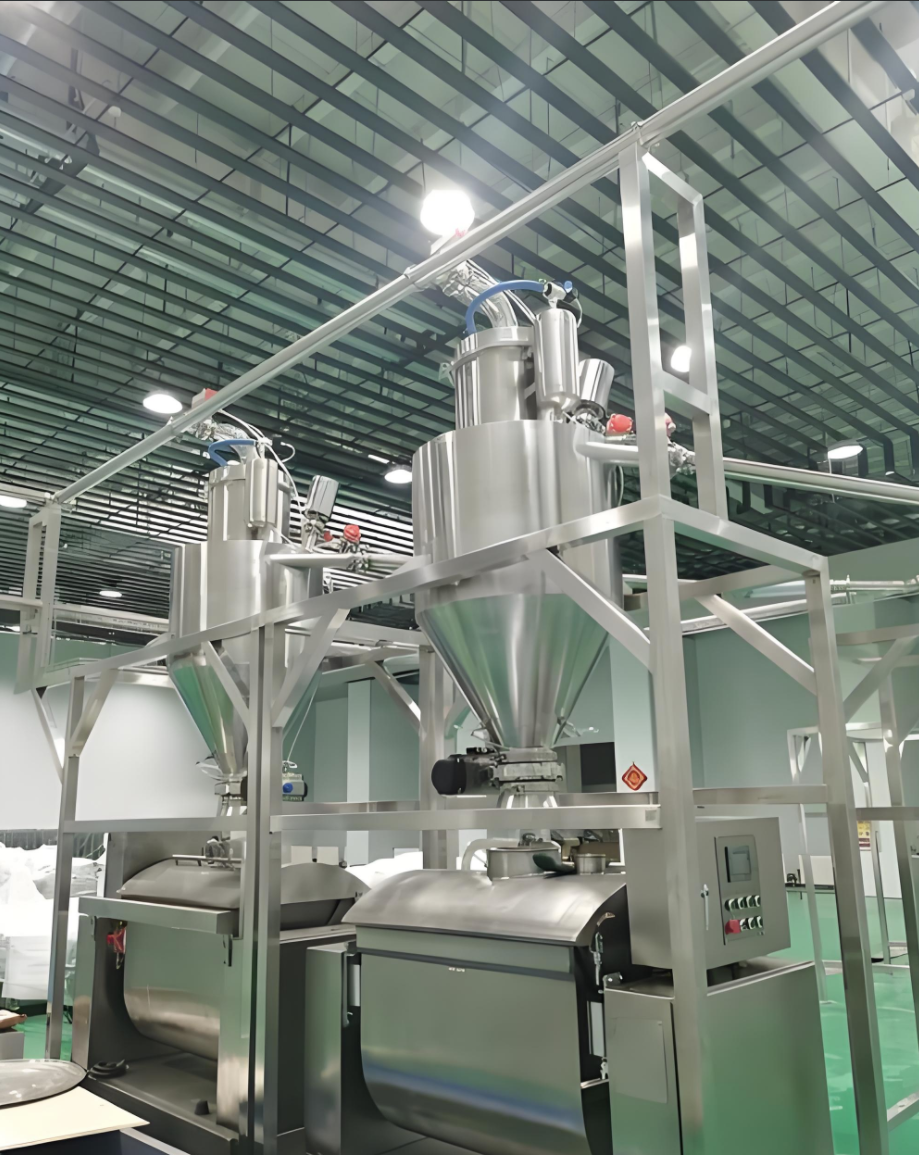
A powder transfer system is a specialized setup used for moving dry powders and granules from one processing stage to another. These systems rely on different technologies such as vacuum, pressure, or mechanical conveyors to ensure safe and efficient material transport without compromising product integrity.
Key Features of a Powder Transfer System:
• Dust-free operation to enhance workplace safety
• Gentle material handling to prevent product degradation
• Automated control to improve efficiency and reduce manual handling
• Compliance with FDA, GMP, and other regulatory standards
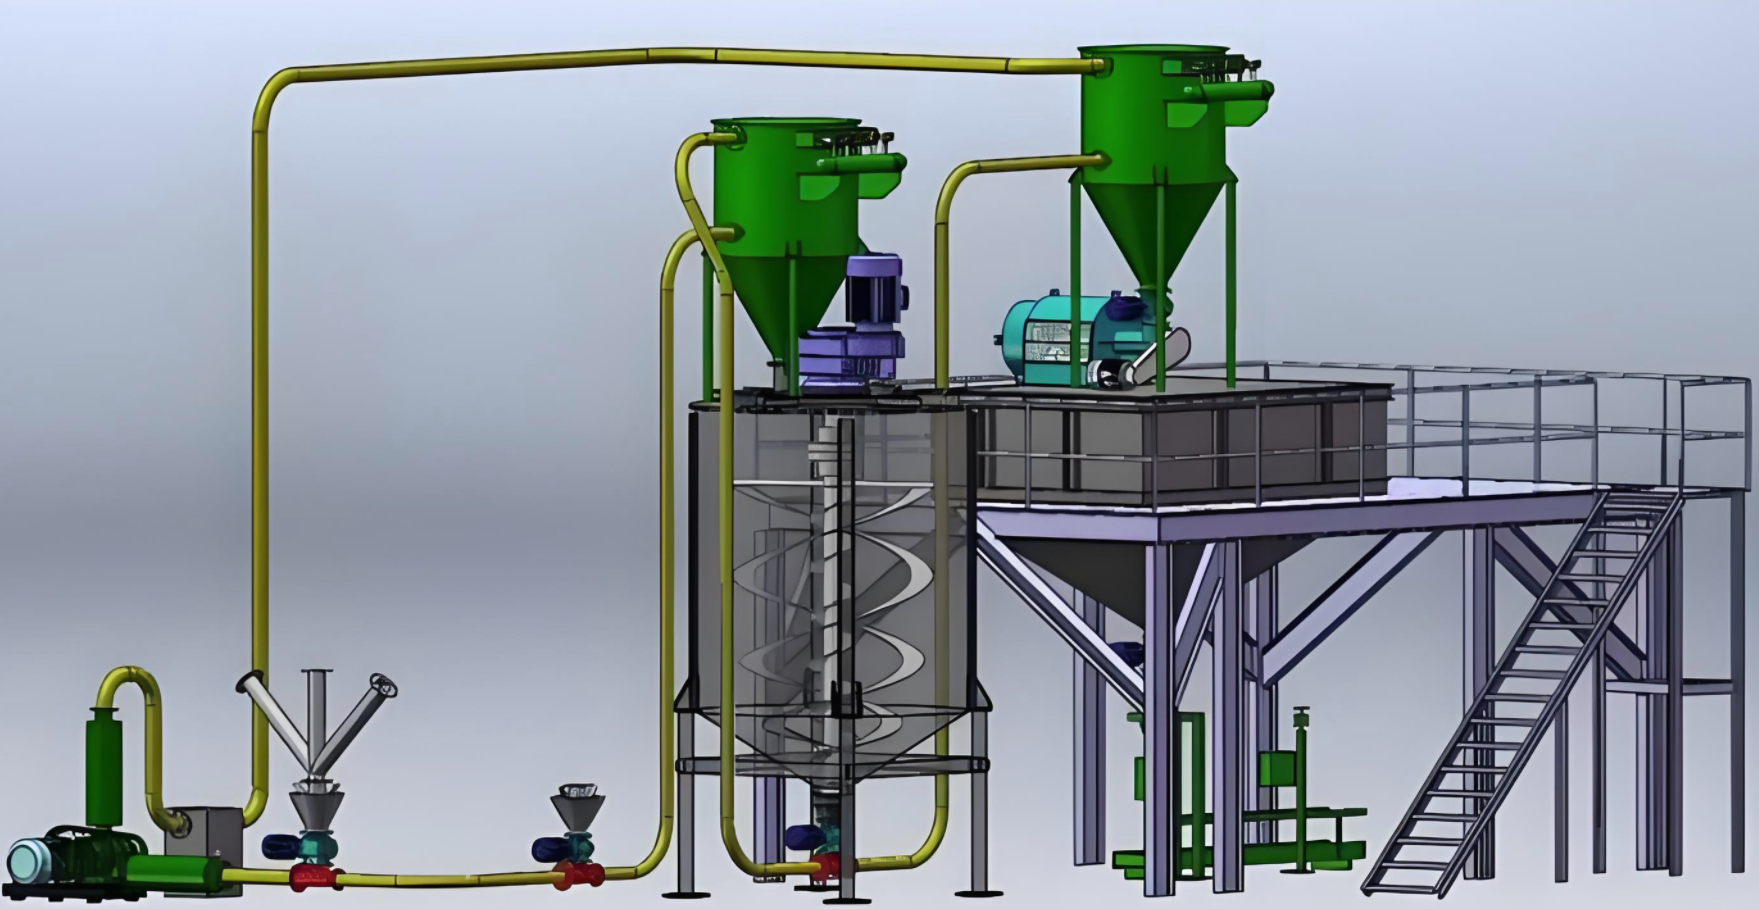
II. Benefits of a Powder Transfer System
• Improved Hygiene & Safety – Minimizes dust exposure, reducing the risk of respiratory hazards and contamination.
• Enhanced Efficiency – Reduces material loss, speeds up production, and eliminates manual powder handling issues.
• Product Integrity – Ensures consistent particle size and prevents segregation or degradation during transfer.
• Regulatory Compliance – Meets industry standards like GMP (Good Manufacturing Practices) for food and pharmaceutical applications.
• Flexibility & Scalability – Suitable for different powder types and can be customized for various production capacities.
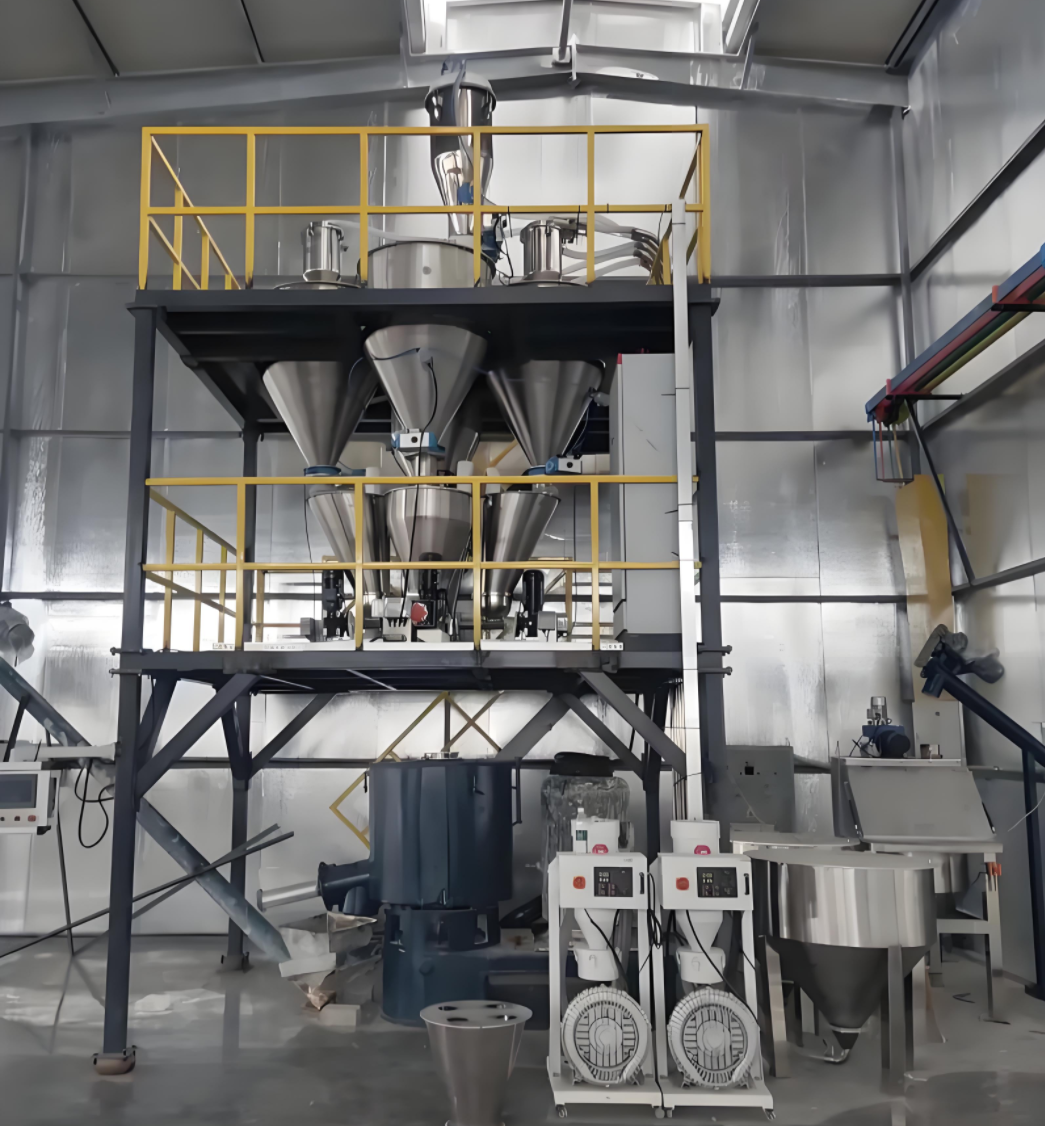
III. Types of Powder Transfer Systems
1. Vacuum Powder Transfer System
How It Works: Uses a vacuum pump to move powders through enclosed pipelines, minimizing contamination.
Best For:
• Pharmaceutical powders (e.g., API, excipients)
• Food industry (e.g., flour, cocoa powder)
• Fine chemical powders
Advantages:
• Hygienic and dust-free operation
• Reduces product waste
• Ideal for fragile powders
2. Pneumatic Powder Transfer System
How It Works: Uses compressed air or inert gases to push powders through pipelines.
Best For:
• Bulk powders in large-scale production
• Industries requiring high-speed transfer
• Powders prone to segregation
Advantages:
• Fast and efficient powder movement
• Handles large quantities with minimal loss
• Reduces cross-contamination risk
3. Mechanical Conveyors (Screw, Belt, or Chain Conveyors)
How It Works: Uses mechanical force (screws, belts, or chains) to transport powders.
Best For:
• Heavy powders (e.g., cement, minerals)
• Continuous production processes
• Industries with limited compressed air availability
Advantages:
• Simple design and easy maintenance
• Cost-effective for certain bulk materials
• Suitable for various industrial applications
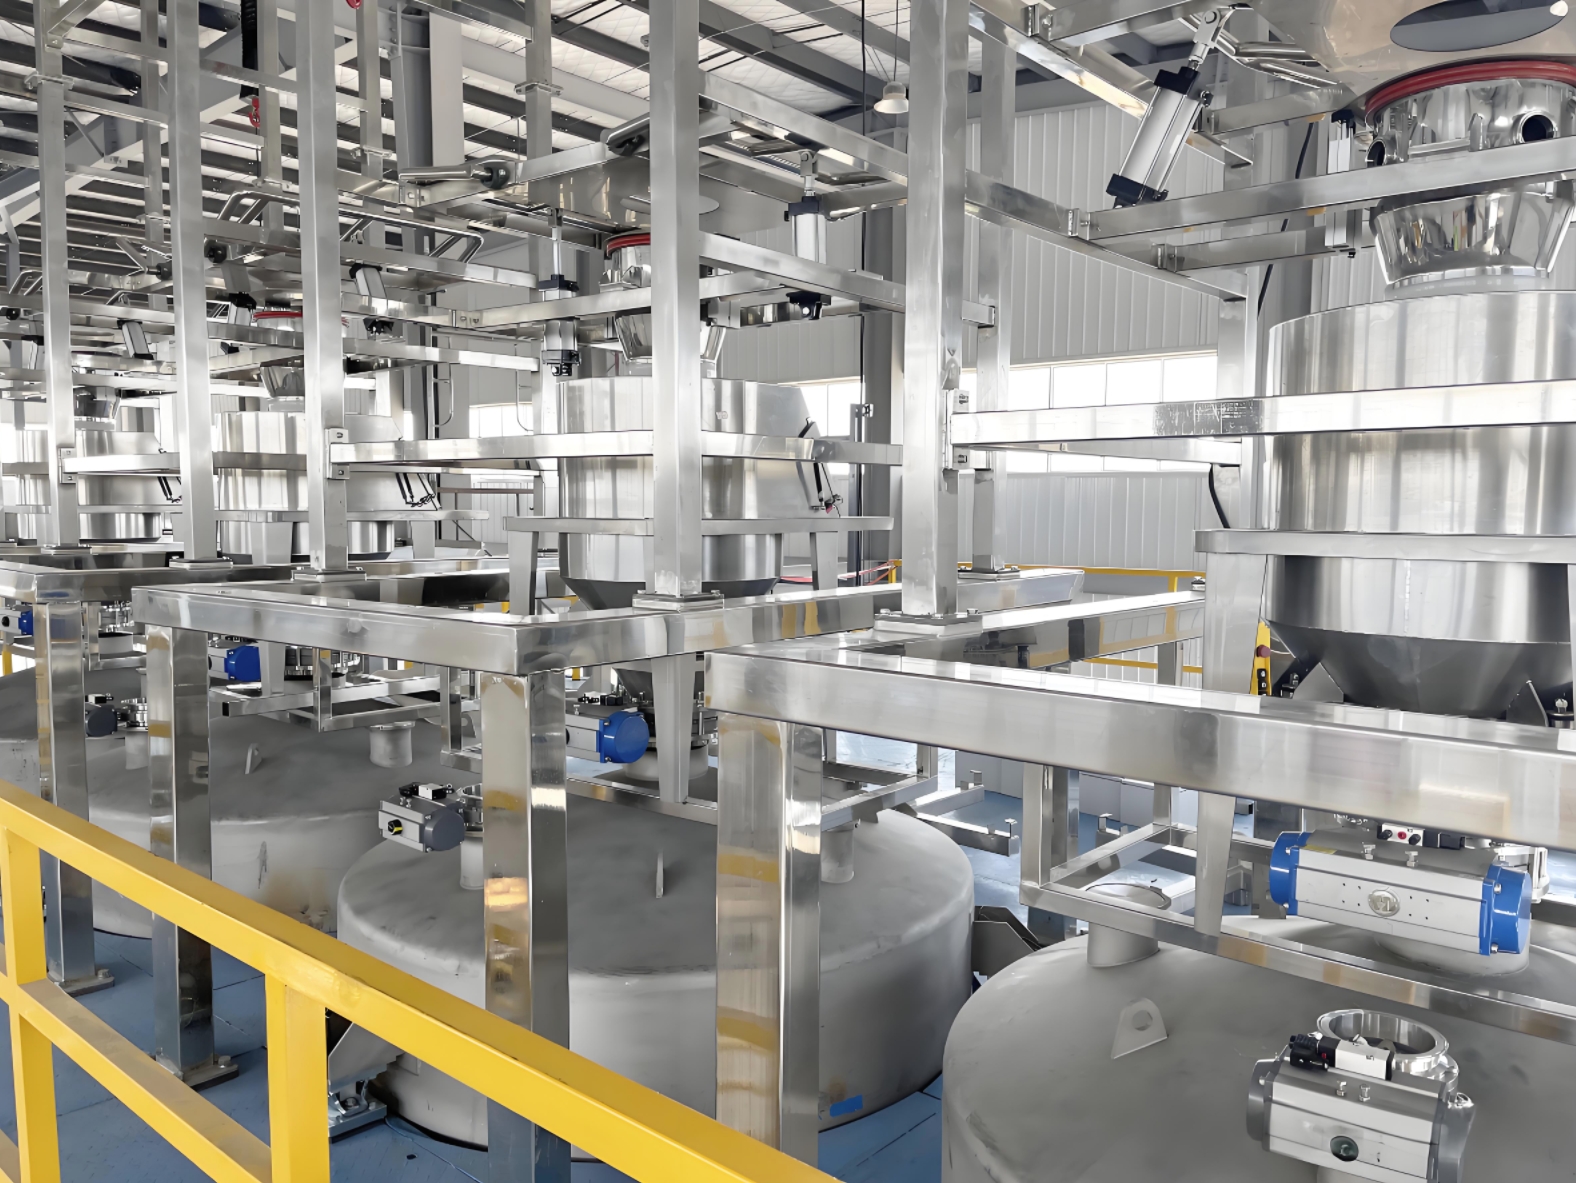
IV. Applications of Powder Transfer Systems
1. Pharmaceutical Industry
• Used for transferring Active Pharmaceutical Ingredients (APIs) and excipients
• Ensures contamination-free handling in cleanroom environments
• Meets GMP and FDA standards for pharmaceutical production
2. Food & Beverage Industry
• Moves ingredients like flour, sugar, and spices in hygienic conditions
• Prevents ingredient cross-contamination
• Supports automated mixing and processing lines
3. Chemical & Petrochemical Industry
• Transfers fine powders like silica, carbon black, and pigments
• Enhances safety by reducing exposure to hazardous chemicals
• Prevents dust explosions with controlled transfer systems
V. How to Choose the Right Powder Transfer System
• Consider Powder Characteristics: Is your material fragile, abrasive, sticky, or hygroscopic? Choose a system that preserves product integrity.
• Production Capacity: Select a system that matches your batch size or continuous production needs.
• Hygiene & Safety Requirements: Ensure compliance with industry regulations like GMP, FDA, or ATEX (for explosive environments).
• Energy Efficiency: Opt for a system that minimizes energy consumption and operational costs.
• Ease of Maintenance: Look for user-friendly systems with minimal downtime and easy cleaning.
VI. Future Trends in Powder Transfer Systems
• Automation & Smart Monitoring: AI-driven powder handling systems improve accuracy, reduce errors, and optimize production.
• Sustainable & Eco-Friendly Designs: Companies are focusing on energy-efficient and low-waste systems to reduce environmental impact.
• Advanced Containment Solutions: High-containment transfer systems help industries like pharmaceuticals maintain sterile and dust-free environments.
Final Thoughts
A well-designed powder transfer system is a game-changer for industries that rely on precise, efficient, and contamination-free powder handling. Whether you’re in pharmaceuticals, food processing, or chemicals, investing in the right system can significantly improve productivity, safety, and regulatory compliance.
• Looking for the best powder transfer solution for your business? Contact us today to find the perfect system for your needs!